
Views: 0 Author: Site Editor Publish Time: 2026-10-18 Origin: Site


The manufacturing of clear plastic components presents one of the most unforgiving environments in the injection molding industry. Whether a facility is producing complex optical lenses, transparent medical diagnostic devices, or premium cosmetic packaging, the margin for error is zero. In this highly specialized field, a microscopic scratch on the cavity seamlessly transfers to the final product. This immediately leads to quality control rejection and skyrocketing scrap rates.
Standard tooling materials frequently degrade over time. They rust and lose their polished luster. Intense heat, extreme injection pressures, and harsh corrosive gases drive this rapid degradation. Tooling engineers must prioritize premium, high-chromium stainless steel alloys to combat these aggressive variables and ensure flawless production runs.
This guide explores the metallurgical science behind achieving optical clarity. We will detail why specific stainless steel grades are an absolute technical requirement. Furthermore, we will examine current industry trends shaping material selection. Finally, we will provide an actionable framework to properly select, process, and maintain tooling steel for high-stakes clear plastic applications.
Optical Clarity Demands Perfection: Clear plastic components require an SPI A-1 or A-2 diamond polish. Any surface defect on the mold cavity instantly causes haze or light distortion on the molded part.
Corrosion Destroys Polish: Transparent resins release highly corrosive byproducts during injection. Utilizing a high-chromium stainless steel is critical to prevent surface pitting.
The Metallurgical Gold Standard: Premium stainless grades provide an optimal balance. They deliver high working hardness, supreme polishability, and excellent natural corrosion resistance.
Global Equivalents: The American AISI 420 standard serves as the equivalent to the German DIN 1.2083 standard. Both offer identical metallurgical benefits for optical molding.
Maintenance Matters: High-quality alloys still require precise vacuum heat treatment, expert diamond polishing, and non-reactive mold releases to survive millions of cycles.
Recent shifts in global manufacturing have made mold steel selection more critical than ever. The automotive industry is aggressively pushing toward lightweighting. Heavy glass headlamps have been replaced with complex, multi-faceted polycarbonate lenses. These modern lenses demand absolute optical perfection to focus LED beams correctly. A subpar mold surface will scatter the light, causing the part to fail strict automotive safety regulations.
Concurrently, the booming medical sector requires flawless transparency for microfluidic chips and diagnostic consumables. Laser reading devices must scan through these plastics without interference. Any microscopic haze from a degraded mold cavity ruins the diagnostic accuracy. In addition, the rising trend of utilizing sustainable, recycled clear resins introduces unpredictable outgassing profiles into the injection barrel. This makes the natural corrosion resistance of the mold cavity an absolute necessity rather than a luxury.
Injection molding relies heavily on the replication effect. Molten polymer is injected into a closed mold cavity under immense pressure. The plastic perfectly mimics the microscopic topography of the steel surface. If the steel is exceptionally smooth and highly reflective, the resulting plastic part shares that exact optical clarity. Conversely, if the steel retains microscopic ridges from CNC machining, the plastic replicates those ridges. This results in a frosted or matte appearance. For transparent components, the mold steel must be polished to a state of near-perfect microscopic flatness.
Uninterrupted light transmission is the primary performance metric in optical applications. Microscopic scratches or subtle orange peel textures on the mold surface act as tiny prisms. They cause light scattering when the plastic part is illuminated. This scattering manifests as hazy or cloudy products. On the shop floor, I have seen technicians pull a massive 5-ton tool from the press simply because a faint haze appeared on a batch of lenses. This light distortion is not just a cosmetic flaw. It is a functional failure that renders the entire batch unusable.
Many people mistakenly believe that any hardened steel can be polished to a mirror shine given enough time. In reality, a true mirror-finish mould steel must possess a pure, uniform, and fine-grained microstructure from the moment it leaves the mill. Non-metallic inclusions, such as microscopic sulfur or phosphorus impurities, cause catastrophic issues during the final polishing phase. When the diamond polishing tool passes over an impurity, it dislodges the softer particle. This leaves behind a microscopic pinhole or comet tail. Optical-grade steels must undergo advanced secondary refinement processes to eliminate these hidden inclusions.
Beyond purity, the hardness of the steel directly dictates its ultimate polishability. Hardness also determines its ability to retain that polish during high-volume manufacturing. A higher hardness allows the steel matrix to be polished to a much higher luster. Elevated hardness prevents the pristine polish from washing out under the high-velocity friction of molten plastic rushing into the cavity.
Standard pre-hardened carbon steels are highly effective for general-purpose, opaque molding. However, they consistently fail in optical applications. They typically max out at a lower hardness, which is simply too soft to hold an SPI A-1 finish over an extended production run. Standard carbon steels also lack the essential chromium content necessary to resist corrosive gases. This leaves them highly susceptible to rapid surface degradation.
Many popular clear thermoplastics become chemically aggressive when subjected to melting temperatures. Polycarbonate, Polymethyl Methacrylate, and especially Polyvinyl Chloride undergo slight thermal degradation. They release acidic gases and volatile organic compounds. This outgassing creates a highly corrosive micro-environment trapped inside the mold cavity during every single shot.
These acidic gases condense on the relatively cooler surface of the mold steel. They immediately initiate a localized chemical attack. If the mold is not constructed from a highly corrosion-resistant material, this acid attack rapidly results in micro-pitting and rust formation. Optical finishes are measured in microns. Even a microscopic layer of oxidation instantly destroys a mirror finish. The resulting clear molded parts turn cloudy and entirely unmarketable.
Relying on inadequate steel for clear parts is a remarkably costly engineering error. Constantly pulling a multi-cavity mold out of the press to manually re-polish the cavity drains profitability. It costs thousands of dollars in machine downtime, specialized maintenance labor, and lost production capacity. Investing in the correct metallurgical foundation upfront mitigates these recurring financial losses entirely.
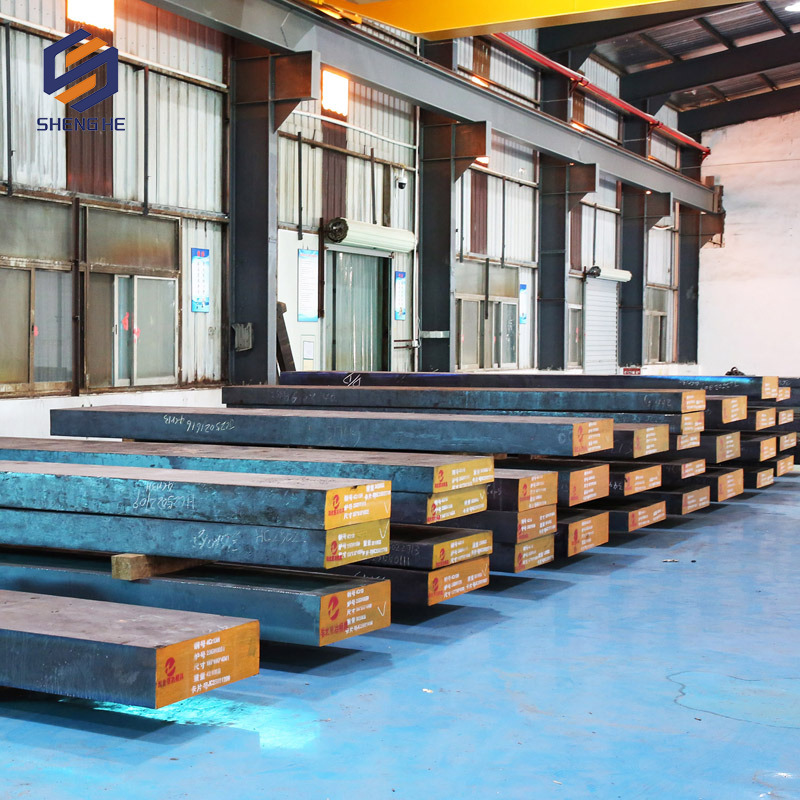
To solve the complex challenges of optical molding, tooling engineers rely on specific martensitic stainless steels. The 1.2083 plastic mold steel is engineered precisely for these demanding environments. It is a highly alloyed, high-carbon, high-chromium stainless steel. It is designed specifically for plastic injection molds that require superior wear resistance combined with an ultra-high-gloss finish.
Procurement managers operating globally often encounter confusion regarding steel nomenclature. Let us clarify the terminology. The designation 1.2083 is the German DIN standard for this specific alloy formulation. In contrast, 420 stainless mold steel serves as the American AISI equivalent. For all practical manufacturing purposes, they represent the exact same family of premium tooling steel.
Standard smelting is rarely sufficient for optical lenses. High-quality optical steel is subjected to Electroslag Remelting. The Electroslag Remelting process slowly remelts the steel ingot drop-by-drop through a reactive chemical slag. This strips away sulfur, phosphorus, and non-metallic inclusions. The result is a highly homogenous, dense microstructure. This makes it the ultimate choice for achieving an SPI A-1 mirror finish without the dreaded risk of pinholing.
To understand why this material is mandatory for clear parts, we must look at the specific metallurgical data. Below is a direct comparison highlighting why standard steels fall short against premium stainless grades.
Technical Parameter | Standard Tooling Steel P20 | Premium 1.2083 / 420 Stainless |
|---|---|---|
Chromium Content | 1.4% to 2.0% | 12.5% to 14.5% |
Carbon Content | 0.28% to 0.40% | 0.36% to 0.42% |
Working Hardness | 28 to 32 HRC | 48 to 52 HRC after vacuum heat treatment |
Corrosion Resistance | Poor. Highly susceptible to outgassing. | Excellent. Forms a passive oxide protective layer. |
Maximum Polish Level | SPI A-3 or B-1 | SPI A-1 Flawless Mirror Finish |
The success of a mirror mold insert is determined at the procurement stage. Engineers must demand comprehensive Ultrasonic Testing reports from their steel supplier. This guarantees the block contains no internal voids or micro-cracks. Verifying Electroslag Remelting quality is non-negotiable. Finding an impurity after hundreds of expensive hours of machining is a devastating scenario.
Premium stainless mold steel is supplied in an annealed state, typically around 235 HB. This softened state allows for efficient CNC rough machining. Once the cavity geometry is cut, the insert must undergo precise vacuum hardening. Heating the steel in a vacuum furnace prevents oxygen exposure. This eliminates surface decarburization and scaling. The tooling engineer's goal is to achieve a uniform working hardness of 50 HRC while minimizing dimensional distortion.
Transforming a machined block into an SPI A-1 mirror finish is a highly specialized art. It begins with meticulous stoning with progressively finer abrasives to erase all directional machine marks. Expert polishers then utilize specialized felt bobs and diamond pastes. They start from coarse grits and carefully step down to 1-micron diamond compounds. Skipping a grit step or applying too much pressure will instantly scratch the steel. The painstaking process must then start over.
High-grade stainless mold steel requires a higher initial capital investment. However, it drastically lowers the Total Cost of Ownership over the tool's lifespan. The upfront premium is rapidly offset by the total elimination of unplanned production stoppages. You avoid constant cavity re-polishing and expensive anti-corrosion treatments. Over a high-volume production cycle, the return on investment is undeniable.
Historically, mold makers utilized cheaper carbon steels and applied a layer of hard chrome plating to provide artificial corrosion resistance. Plating adds physical thickness, which alters the critical dimensional accuracy of the optical cavity. Furthermore, plating often flakes under high injection pressures. Premium stainless grades are naturally corrosion-resistant throughout their entire core. Engineers can completely bypass the risky and dimension-altering chrome plating process.
Even the most perfectly polished steel can be compromised by incorrect shop-floor chemicals. Standard aerosol mold releases contain additives that react with the hot steel surface. They leave behind a stubborn, baked-on microscopic residue. This residue transfers to the clear plastic, causing a cloudy defect. Maintenance teams must strictly utilize non-reactive, optical-safe mold releases formulated specifically for transparent resins.
When a production run concludes, the mold cavity must be meticulously cleaned. Technicians should only use dedicated optical solvents and specialized microfiber wipes. Wiping a mirror cavity with a standard shop rag will introduce micro-scratches immediately. To protect the finish in humid warehouse environments, a light, moisture-displacing preventative oil should be carefully applied before the tool is closed.
Manufacturing optically clear plastic components leaves zero room for compromised tooling. The visual perfection and light transmission of the final product are directly tied to the metallurgical quality of the mold cavity. Relying on sub-standard materials inevitably results in surface degradation and unacceptable scrap rates.
Investing in high-purity, martensitic stainless steel is the most scientifically proven method to ensure a durable mirror finish. By prioritizing the right material upfront and adhering to strict processing protocols, manufacturers guarantee flawless production runs. If you are designing a tool for clear plastics, source your materials carefully. Visit Shenghe Steel today to explore our full range of premium, ESR-refined plastic mold steels engineered specifically for flawless optical clarity.
No. Lower-grade carbon steels naturally contain non-metallic impurities. When subjected to diamond polishing, the friction dislodges these impurities. This causes microscopic pinholes or a wavy orange peel texture on the surface. Only high-purity, specially refined steels can achieve a true, flawless mirror finish suitable for optical replication.
Both are highly regarded martensitic stainless mold steels. The primary metallurgical difference is that 1.2316 contains added Molybdenum. This provides even higher corrosion resistance, making it preferred for highly corrosive resins like pure Polyvinyl Chloride. However, 1.2083 generally offers superior high-gloss polishability due to its specific microstructure. This makes it the better option for optical clear parts like lenses.
In its pre-delivery annealed state from the steel mill, it measures around 235 HB. This is soft enough for standard CNC machining. After the cavity geometry is fully machined, the block undergoes vacuum heat treatment. This thermal process allows the steel to achieve a final working hardness of 48 to 52 HRC. This is the ideal hardness range for holding an SPI A-1 mirror polish under high injection pressures.
Generally, no. This specific stainless grade contains up to 14.5% chromium. It boasts excellent inherent natural corrosion resistance. This built-in chemical property eliminates the need for costly and dimension-altering hard chrome plating. It simplifies the mold-making process while ensuring long-term durability against acidic resin outgassing.
The lifespan of a mirror finish depends entirely on the steel's hardness and the resin being injected. A premium stainless steel hardened to 50 HRC can maintain an SPI A-1 finish for hundreds of thousands of cycles when shooting clean, non-glass-filled resins like Polycarbonate. Routine preventative maintenance and gentle cleaning are required to maximize this lifespan.
Cloudiness is almost always a surface replication issue. If the mold steel has degraded due to acidic outgassing, rust, or micro-scratches from improper cleaning, the plastic will mold into those microscopic defects. The rough surface scatters light, causing the part to look cloudy. Upgrading to a highly polished, corrosion-resistant stainless steel cavity resolves this issue.


